If you've ever looked at the ingredient list of your serum, eye drops, or joint supplement, chances are you've seen "sodium hyaluronate" — the stable, water-soluble salt form of hyaluronic acid. But have you ever wondered how this remarkable molecule actually gets made?
The answer matters more than you might think. The manufacturing process doesn't just determine the cost of the raw material — it directly affects purity, molecular weight distribution, safety, and ultimately, how well the ingredient performs in your final product.
This guide walks through the complete manufacturing journey of sodium hyaluronate, from strain selection to finished powder, and explains why each step matters if you're sourcing this ingredient for pharmaceutical, cosmetic, food, or industrial applications.
A Brief History: From Rooster Combs to Bioreactors
The story of hyaluronic acid begins in 1934, when Columbia University ophthalmologist Karl Meyer and his assistant John Palmer isolated a novel polysaccharide from bovine vitreous humor. They named it "hyaluronic acid" — combining the Greek "hyalos" (glass/vitreous) with "uronic acid."
For the next several decades, extraction from animal tissues was the only option. The primary sources were rooster combs (containing roughly 0.3%–0.8% hyaluronic acid by weight), bovine vitreous bodies, and shark cartilage. While this approach yielded a "natural" substance, it came with serious limitations:
· Scarce raw materials — supply depended on livestock availability and seasonal fluctuation
· Complex extraction — multiple solvent washes, enzymatic treatments, and chromatographic steps were needed
· Inconsistent purity — residual proteins and animal-derived contaminants were difficult to eliminate
· Disease transmission risk — animal-sourced materials carried potential pathogen concerns
· Prohibitive cost — production volumes were tiny, restricting use to niche medical applications
The breakthrough came in the 1980s when researchers developed microbial fermentation methods to produce hyaluronic acid at scale. By the early 2000s, fermentation had become the dominant production method. Today, over 99% of the world's sodium hyaluronate is manufactured through bacterial fermentation — a shift that transformed this once-exotic ingredient into a widely accessible raw material powering a multi-billion-dollar global market.
Step 1 — Strain Selection: The Foundation of Quality
Every batch of sodium hyaluronate starts with a single decision: which microorganism will produce it?
The Traditional Workhorse: Streptococcus zooepidemicus
The most widely used production organism is Streptococcus zooepidemicus, a non-pathogenic subspecies of Streptococcus equi. This bacterium naturally synthesizes a polysaccharide capsule composed of hyaluronic acid, making it an efficient biological factory. Industrial strains have been carefully selected and attenuated over decades to remove hemolytic activity while maximizing HA yield.
The advantage of streptococcal strains is their proven track record: they reliably produce high-molecular-weight HA (often exceeding 1–2 MDa) at titers of 2.5–7 g/L in optimized fermentation conditions.
Next-Generation Hosts: GRAS-Class Alternatives
Because streptococcal species carry inherent concerns about potential endotoxin contamination from pathogenic relatives, the industry has invested heavily in "GRAS" (Generally Recognized As Safe) alternative hosts:
· Bacillus subtilis — Recombinant strains expressing the hasA gene (hyaluronan synthase) from streptococci, combined with native precursor genes (tuaD, gtaB, hasB). Novozymes notably developed a B. subtilis process yielding up to 5 g/L of HA with molecular weights of 1–1.2 MDa in sucrose-based media.
· Lactococcus lactis — A food-grade lactic acid bacterium. Through the nisin-controlled expression system (NICE), researchers achieved HA yields of 1.8 g/L in aerated bioreactors.
· Escherichia coli — Engineered strains expressing pmHAS from Pasteurella multocida have reached yields up to 3.8 g/L with molecular weights up to 1.5 MDa.
· Streptococcus thermophilus — A dairy-associated, non-pathogenic thermophile that can produce HA from lactose, opening interesting possibilities for food-grade applications.
Why this matters for your product: The host organism determines the baseline safety profile, the achievable molecular weight range, and the downstream purification complexity. A manufacturer's strain selection strategy reveals a great deal about their commitment to quality and regulatory compliance.
Step 2 — Fermentation: Where Molecules Are Born
Once the right strain is selected and cultivated through a seed train (typically 3 stages with 10× expansion at each level), the production fermentation begins.
The Fermentation Environment
The bacteria are inoculated into large-scale sterile bioreactors containing a carefully formulated culture medium:
· Carbon source: Glucose or sucrose (typically 25–50 g/L) — the building block for HA chain synthesis
· Nitrogen source: Yeast extract and/or peptone (30–60 g/L) — supporting cell growth and metabolism
· Minerals and salts: Phosphate, magnesium, potassium, and trace elements (approximately 11 g/L)
· Aeration: 2.0 VVM (volumes of air per volume of liquid per minute) of sterile air — even though S. zooepidemicus is a facultative anaerobe, oxygen helps generate reducing equivalents needed for HA synthesis
Critical Process Parameters
Parameter | Typical Value | Impact on Product |
Temperature | 37°C | Affects growth rate and enzyme activity |
pH | 7.0 (controlled with NaOH) | Influences molecular weight and yield |
Dissolved oxygen | Aerated at 2.0 VVM | Supports metabolic activity |
Fermentation duration | 24–48 hours | Determines final titer and MW distribution |
Batch vs. Fed-Batch: A Key Decision
The fermentation mode significantly affects output:
· Batch fermentation: Simpler to operate, typical titers around 2.5 g/L after 24 hours
· Fed-batch fermentation: Nutrients are fed incrementally, achieving titers of 5.0 g/L or higher, with better control over molecular weight distribution
· Continuous fermentation: Emerging approach with potential for even higher productivity, though less commonly adopted industrially
Why this matters for your product: The fermentation step is where the molecular weight distribution of the final product is largely determined. Temperature, pH, aeration, and feeding strategy all influence whether the resulting HA has a molecular weight of 50 kDa (suitable for skin penetration) or 2.5 MDa (ideal for viscoelastic applications like ophthalmic surgery). Consistent fermentation control is the difference between batch-to-batch reliability and unpredictable quality variation.
Step 3 — Recovery & Purification: The Quality Bottleneck
When fermentation ends, you have a complex broth containing hyaluronic acid, bacterial cells, residual proteins, nucleic acids, organic acids, and spent medium components. Transforming this into a pure, safe, specification-compliant product requires a sophisticated purification cascade.
Cell Removal
The first step is separating the HA-rich supernatant from the bacterial biomass:
1. Disk-stack centrifugation — Removes approximately 97% of cells, producing a wet solids stream and clarified supernatant
2. Dead-end microfiltration (0.22 μm) — Captures residual cells, ensuring a particle-free filtrate
Concentration and Diafiltration
The clarified filtrate then passes through tangential flow filtration (TFF) using a membrane with a molecular weight cut-off (MWCO) typically at 100 kDa:
· The HA polymer (being much larger than 100 kDa) is retained by the membrane
· Small molecules — salts, residual sugars, lactate, acetate — pass through
· Multiple diafiltration cycles with deionized water further reduce impurity levels
· Product yield in this step: approximately 96%
Protein and Nucleic Acid Removal
This is where product grade differentiation becomes critical:
· Activated carbon adsorption — Granular activated carbon (GAC) columns bind residual proteins, nucleic acids, pigments, and other organic impurities while allowing ~99% of HA to pass through
· Enzymatic treatment — Some manufacturers use proteases to degrade residual proteins before filtration
· Additional ultrafiltration steps — Further reduce protein content to meet pharmacopeial limits
Precipitation and Recovery
The purified HA solution is then precipitated:
· Alcohol precipitation — Addition of ethanol or isopropanol (typically to ~42% v/v final concentration) causes the HA to precipitate as a fibrous white mass
· Basket centrifugation — Separates the HA precipitate from the alcohol supernatant
· Washing — The precipitate is washed with additional alcohol to remove residual salts and impurities
· Precipitation yield: approximately 95%
The Grade Divergence Point
This is where manufacturing paths diverge based on the target application:
Quality Parameter | Cosmetic Grade | Food Grade | Ophthalmic/Injectable Grade |
Protein content | ≤0.5% | ≤0.5% | ≤0.1% (European Pharmacopoeia) |
Endotoxin level | Standard control | Standard control | <0.05–0.5 EU/mg |
Additional purification | Standard | Standard | Extended TFF (1000 kDa MWCO), WFI diafiltration, sterile filtration |
Drying method | Spray drying acceptable | Spray drying acceptable | Lyophilization (freeze-drying) preferred |
Sterility assurance | Not required | Not required | 0.22 μm sterile filtration + aseptic processing |
For ophthalmic and injectable grades, approximately 10% of the purified HA precipitate may be diverted to an additional ultra-fine purification line involving a second TFF step at 1000 kDa MWCO, diafiltration with water for injection (WFI), sterile filtration, and lyophilization.
Why this matters for your product: Purification is the single most consequential step in determining final product quality. Inadequate protein removal leads to immunogenicity risks. Insufficient endotoxin control makes the material unsuitable for injectable or ophthalmic use. A manufacturer's purification capability — not their fermentation volume — is often the true bottleneck and the most meaningful differentiator.
Step 4 — Drying, Milling & Packaging: The Final Touch
The purified HA precipitate or solution must be converted into a stable, easily handled solid form.
Drying Methods
Method | Temperature | Pros | Cons | Best For |
Spray drying | High (150–200°C inlet) | Fast, efficient, low cost | Thermal degradation of high-MW HA | Cosmetic/food grade |
Vacuum drying | Moderate (40–60°C) | Gentler on molecular weight | Slower, less uniform | General pharmaceutical |
Lyophilization (freeze-drying) | Low (−20°C to −40°C) | Best MW preservation, excellent solubility | Highest cost, longest cycle | Injectable/ophthalmic grade |
The choice of drying method directly affects:
· Molecular weight retention — High temperatures can break polymer chains, reducing MW
· Dissolution rate — Lyophilized products dissolve faster and more completely
· Moisture content — Proper drying ensures stability during storage (typically <10% weight loss on drying)
· Powder characteristics — Particle size, flowability, and bulk density
Milling and Sieving
After drying, the material is milled (often using jet milling to minimize thermal degradation) and sieved to achieve uniform particle size distribution. This step ensures consistent flowability and dissolution behavior in downstream formulation.
Packaging
Final packaging follows strict protocols:
· Aseptic double-layer polyethylene bags under nitrogen atmosphere (for pharmaceutical grades)
· Standard moisture-proof packaging for cosmetic and food grades
· Storage recommendations: sealed, protected from light and moisture; pharmaceutical grades often stored at 2–8°C
Why this matters for your product: Improper drying can degrade molecular weight — the very property you may be paying a premium for. Inadequate packaging leads to moisture absorption, clumping, and microbial growth during storage. These may seem like "boring" final steps, but they're where otherwise excellent product can be compromised.
How to Evaluate a Sodium Hyaluronate Manufacturer
Understanding the manufacturing process gives you a powerful framework for evaluating potential suppliers. Here are the five critical dimensions to assess:
1. Strain Portfolio and Safety Management
· Does the manufacturer use well-characterized, attenuated strains?
· Have they invested in GRAS-class hosts (e.g., B. subtilis) for added safety assurance?
· Can they provide documentation on strain safety testing?
2. Fermentation Scale and Batch Consistency
· What is their fermentation capacity? (World-class facilities operate 30–4000 L reactors with multiple production lines)
· Do they use fed-batch or advanced continuous fermentation for better consistency?
· What is their batch-to-batch molecular weight coefficient of variation?
· Can they reliably produce across the full molecular weight spectrum (from 5 kDa to 2.5+ MDa)?
3. Purification Capability
· Can they achieve pharmacopeial-grade purity (protein ≤0.1%, endotoxin <0.05 EU/mg)?
· Do they have dedicated purification lines for different application grades?
· What is their ultrafiltration and diafiltration capacity?
4. Quality System and Certifications
· ISO 13485 (medical device quality management)?
· CEP/DMF filings with regulatory agencies (FDA, EMA)?
· COSMOS certification for natural/organic cosmetics?
· HALAL, SGS, cGMP compliance?
· Full batch traceability and Certificate of Analysis (COA) for every lot?
5. Technical Support and Customization
· Can they customize molecular weight to your specific application needs?
· Do they offer different grades (cosmetic, food, ophthalmic, injectable) from the same manufacturing platform?
· Can they provide regulatory support for your product registration in target markets?
Red flags to watch for: Inability to provide complete COAs, no batch-to-batch traceability, absence of endotoxin testing, vague descriptions of strain sources, or reliance on third-party manufacturing without direct quality oversight.
The Manufacturing Advantage: Why Process Expertise Matters
The journey from a single bacterial cell to a kilogram of pharmaceutical-grade sodium hyaluronate powder involves hundreds of controlled steps, each one carrying the potential to either preserve or compromise product quality.
Fermentation determines the molecular foundation. Purification defines the safety boundary. Drying and packaging determine the shelf-life reality. And the quality system tying everything together determines whether you can trust every batch that arrives at your door.
This is why choosing a manufacturer with deep process expertise — not just a competitive price — matters so profoundly for your product's success.
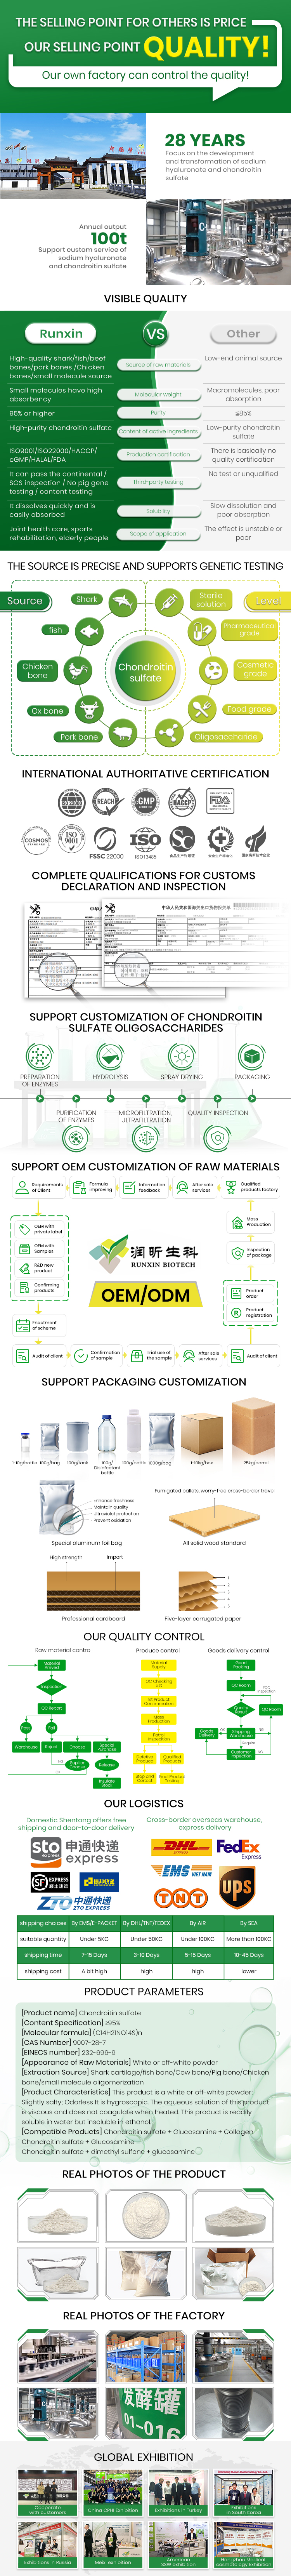
Companies like Shandong Runxin Biotechnology exemplify what world-class SH manufacturing looks like in practice. With 28 years of dedicated hyaluronic acid research and production, Runxin operates a fully integrated manufacturing platform — from strain development through fermentation, purification, drying, and packaging — entirely in-house. Their facility delivers daily production capacity exceeding 100,000 units, supported by a comprehensive certification portfolio including ISO 13485, CE, DMF (036368), COSMOS, HALAL, SGS, and cGMP. Export experience spanning 34 countries demonstrates the kind of regulatory fluency and quality consistency that global brands require.
In a market where sodium hyaluronate has become a commodity ingredient, the differentiator isn't just the molecule itself — it's the depth of manufacturing expertise behind every batch. Whether you're formulating a premium skincare serum, developing an ophthalmic solution, or scaling a joint health supplement, the manufacturing process is where quality is either built in or designed out.
Choose your manufacturer as carefully as you choose your formulation.
Looking for a reliable sodium hyaluronate supplier? Contact Runxin Biotechnology to learn more about our full-spectrum manufacturing capabilities, from cosmetic-grade to injectable-grade sodium hyaluronate, backed by 28 years of fermentation expertise and global regulatory compliance.