If you've ever received a Certificate of Analysis for sodium hyaluronate and felt overwhelmed by the list of parameters — protein, nucleic acids, endotoxin, heavy metals, loss on drying — you're not alone. Most suppliers present these numbers as a simple pass/fail checklist. But purity is far more nuanced than a single percentage.
Here's the short answer: purity is not one number — it's a multi-dimensional profile. A supplier claiming "99% purity" without specifying which impurities were tested, at what detection limits, and by which methods, is giving you incomplete information at best.
For B2B buyers, formulators, and quality control professionals, understanding what purity actually means for hyaluronic acid — and how each dimension is measured — is essential for ensuring your final product is safe, effective, and consistent. Let's break it down.
What "Purity" Actually Means — It's Not Just One Number
When someone says "sodium hyaluronate purity," they're usually referring to three distinct dimensions, each measuring something fundamentally different:
Chemical Purity measures how much of the material is actually sodium hyaluronate versus other chemical substances. This is typically expressed as:
· Assay (HA content): The percentage of sodium hyaluronate on a dry basis. Cosmetic grade typically requires ≥90.0%, while pharmaceutical grade requires ≥95.0%.
· Glucuronic acid content: A structural component of HA. The theoretical value is ~46%, so a result ≥44% confirms the HA chain structure is intact.
Biological Safety Impurities are the most critical for applications that contact living tissue:
· Residual proteins: Leftover from the fermentation host organism. These are the primary allergen risk.
· Nucleic acids (DNA/RNA): Also from the host organism. High levels indicate incomplete purification.
· Bacterial endotoxins: Lipopolysaccharides from gram-negative bacteria. Critical for injectable and ophthalmic applications.
· Microbial contamination: Total aerobic count, yeast/mold, and specific pathogens.
Chemical Impurities come from the manufacturing process and environment:
· Heavy metals: Lead, arsenic, cadmium, mercury — regulated at ppm levels.
· Residual solvents: Methanol, ethanol, isopropanol from the purification steps.
· Iron, chloride, sulfate: Inorganic contaminants from equipment or water.
Think of it like a medical checkup: your total health isn't defined by a single blood test result. It's the combination of all markers — blood pressure, cholesterol, liver function, kidney function — that tells the full story. Sodium hyaluronate purity works the same way.
Where Impurities Come From: Fermentation vs. Extraction
The source of your sodium hyaluronate determines which impurities you need to worry about.
Traditional Extraction (Animal Source)
Historically, hyaluronic acid was extracted from rooster combs or bovine vitreous humor. This method carries specific impurity risks:
· Animal-source proteins that can trigger immune responses
· Sulfate residues (unlike HA, chondroitin sulfate contains sulfate groups)
· Batch-to-batch variability depending on the animal source
· Limited scalability
Most commercial production has shifted away from animal extraction for these reasons, though some niche suppliers still use this method.
Microbial Fermentation (Current Standard)
Modern sodium hyaluronate is produced by fermenting bacteria — typically Streptococcus equi subsp. zooepidemicus or engineered Bacillus subtilis strains. This eliminates animal-source risks but introduces its own impurity profile:
· Host organism proteins: The bacteria produce proteins alongside HA during fermentation.
· Nucleic acids: Bacterial DNA and RNA co-exist with HA in the fermentation broth.
· Fermentation media components: Sugars, amino acids, and minerals from the growth medium.
· Endotoxins: If gram-negative bacteria are present as contaminants.
The purification process — precipitation, ultrafiltration, chromatography — is what separates a high-purity product from a commodity lot. Suppliers who cut corners on purification will show elevated protein and nucleic acid levels, even if the HA assay percentage looks acceptable.
How Purity Is Tested: The Core Methods
Each impurity category requires a specific analytical method. Here's what's actually happening in the lab:
HA Content / Glucuronic Acid
Carbazole colorimetric method: The most traditional approach. HA is hydrolyzed to release glucuronic acid, which reacts with carbazole reagent to produce a purple color. The intensity is measured by spectrophotometry and compared to a standard curve. Simple, inexpensive, but can be affected by other uronic acids.
CTAB turbidimetric method: Cetyltrimethylammonium bromide forms a complex with HA, creating turbidity proportional to HA concentration. Faster than carbazole but less specific.
HPLC-SEC (Size-Exclusion Chromatography): Separates HA molecules by size before detection. This is the gold standard because it simultaneously confirms HA identity and quantifies it. It also reveals the molecular weight distribution — information that a simple assay number cannot provide.
Residual Protein
This is arguably the most important purity indicator for safety.
Bradford method (595 nm): Uses Coomassie Brilliant Blue G-250 dye that binds to proteins. When measured at 595 nm with a BSA (bovine serum albumin) calibration curve, it provides reliable quantification down to 0.005% (w/w). This is the preferred method because it's not interfered with by HA's own UV absorption.
Lowry method: Similar sensitivity to Bradford but more complex protocol with multiple reagent additions.
UV 280 nm absorbance: The simplest method but least reliable. HA itself absorbs some UV at 280 nm, which can cause false positives and undercounting of actual protein content. If a supplier only reports UV 280 nm protein data, be cautious.
The cosmetic industry standard is ≤0.1% residual protein. Pharmaceutical and injectable grades require ≤0.05%. A well-controlled fermentation process typically produces protein levels below 0.05%, but we've seen data from the same supplier swinging from 0.02% to 0.18% across different batches — a clear indicator of inconsistent purification.
Nucleic Acids
UV 260 nm absorbance: DNA and RNA absorb strongly at 260 nm. The sample is dissolved and the absorbance is measured directly. A reading above 0.1 (Abs) suggests incomplete purification. While nucleic acids don't pose a direct safety risk in topical cosmetics, elevated levels correlate with higher endotoxin loads — so this is a useful process control indicator.
Bacterial Endotoxin
LAL (Limulus Amebocyte Lysate) method: Uses lysate from horseshoe crab blood cells, which clot in the presence of endotoxins. The reaction can be measured kinetically (dynamic turbidimetric or chromogenic) for quantitative results. This is the only accepted method for injectable and ophthalmic grade products.
The typical limit is ≤0.5 EU/mg for raw material powder. Injectable applications require even stricter control.
Heavy Metals
ICP-MS (Inductively Coupled Plasma Mass Spectrometry): The most sensitive method, capable of detecting metals at parts-per-billion levels. Tests for lead (Pb), arsenic (As), cadmium (Cd), mercury (Hg), and often additional elements.
Atomic Absorption Spectroscopy (AAS): Specifically used for iron content, which requires a different detection wavelength (248.3 nm).
Typical limits: Heavy metals (as Pb) ≤20 ppm for cosmetic grade, ≤10 ppm for pharmaceutical grade. Arsenic ≤3 ppm, cadmium ≤1 ppm, mercury ≤0.1 ppm.
Residual Solvents
Headspace Gas Chromatography (GC): The sample is heated in a sealed vial, and volatile compounds in the headspace are analyzed by GC. This detects methanol, ethanol, and isopropanol residues from the purification and precipitation steps.
The Chinese Pharmacopoeia specifies these limits for pharmaceutical-grade sodium hyaluronate. If a supplier uses ethanol precipitation (the most common method), residual ethanol testing is essential.
Microbial Limits
Standard plate count methods per USP <61> and <62>:
· Total aerobic microbial count: ≤100 cfu/g (cosmetic), ≤10⊃2; cfu/g (pharmaceutical)
· Yeast and mold: ≤100 cfu/g
· Specific pathogens: Staphylococcus aureus, Pseudomonas aeruginosa, E. coli must be absent
· For fermentation-derived products: additional testing for hemolytic streptococcus
Reading a COA: What to Check and What the Numbers Mean
A typical Certificate of Analysis for sodium hyaluronate includes 15-20 parameters. Here's how to read the most critical ones:
Specification Comparison by Grade
Parameter | Cosmetic Grade | Food/Supplement Grade | Pharmaceutical / Injectable Grade | Test Method |
Assay (dry basis) | ≥90.0% | ≥91.0% | 95.0–105.0% | Carbazole / HPLC |
Protein residual | ≤0.1% | ≤0.05% | ≤0.05% | Bradford / Lowry |
Nucleic acids | ≤0.1% | ≤0.1% | ≤0.05% | UV 260 nm |
Heavy metals (as Pb) | ≤20 ppm | ≤10 ppm | ≤10 ppm | ICP-MS |
Endotoxin | Not always tested | Not always tested | ≤0.05 EU/mg | LAL |
Loss on drying | ≤10.0% | ≤10.0% | ≤10.0% | 105°C / 60°C vacuum |
pH (1% solution) | 5.0–8.5 | 6.0–7.5 | 6.0–7.5 | Potentiometric |
Clarity & color | Clear, A₆₀₀≤0.01 | Clear, A₆₀₀≤0.01 | Clear, A₆₀₀≤0.01 | UV spectrophotometry |
Residual solvents | Not always tested | Methanol ≤0.05%, Ethanol ≤0.5% | Per pharmacopoeia | Headspace GC |
Specific rotation | — | — | +60° to +80° | Polarimetry |
Red Flags on a COA
Protein >0.1% in cosmetic grade: Indicates inadequate purification. Increases allergy risk, especially for leave-on products and sensitive skin formulations.
Missing endotoxin data for injectable/ophthalmic claims: If a supplier markets their product for injection or eye drop applications but doesn't test endotoxin, the product is not suitable for those uses regardless of other specifications.
No molecular weight distribution data: A single "average MW" number tells you nothing about the actual chain length distribution. A PDI (polydispersity index) above 2.0 indicates significant batch heterogeneity.
Missing specific pathogen testing: Total plate count alone is not sufficient. The absence of S. aureus, P. aeruginosa, and E. coli must be confirmed separately.
Assay at exactly the specification limit: If the assay reads exactly 90.0% for cosmetic grade, it may indicate the product was blended to just meet the minimum — rather than being a naturally high-purity batch.
Why Purity Matters for Your Final Product
Purity isn't an abstract quality metric — it directly impacts your product's safety, efficacy, and market compliance.
Safety
Residual proteins are the primary allergenic risk in sodium hyaluronate. For products applied to compromised skin (post-procedure, wound care, sensitive skin), protein levels above 0.1% can trigger immune responses. Endotoxin contamination in injectable products can cause serious inflammatory reactions — this is why the LAL test is non-negotiable for ophthalmic and injectable applications.
Efficacy
Impurities can interfere with hyaluronic acid's biological activity. Residual nucleic acids and degraded HA fragments can activate inflammatory pathways (TLR2/TLR4) instead of the desired CD44-mediated anti-inflammatory signaling. In essence, impure HA may do the opposite of what you intended.
Formulation Stability
Metal ions (especially iron) catalyze oxidative degradation of hyaluronic acid chains, reducing molecular weight over time. If your product's viscosity drops during storage, residual iron or other metal contaminants may be the cause. Similarly, microbial contamination introduces hyaluronidase activity that breaks down hyaluronic acid.
Regulatory Compliance
Different markets have different requirements:
· USA: Must meet USP standards for pharmaceutical applications
· EU: Must comply with EP monograph 0338
· China: Must comply with Chinese Pharmacopoeia standards
· Cosmetics: Generally less regulated, but responsible brands should still require full impurity testing
Batch Consistency
Perhaps the most commercially significant issue: purity fluctuation between batches forces you to reformulate or reject incoming material. A supplier whose protein levels swing between 0.02% and 0.18% is a supplier whose fermentation and purification processes are not under control — even if every individual batch technically "passes."
How to Evaluate Your Supplier's Purity Capabilities
When assessing a sodium hyaluronate supplier, focus on these five dimensions:
1. Testing Methods
Ask specifically: What method do you use for protein testing? If the answer is UV 280 nm only, that's a gap. Bradford or Lowry at minimum. For molecular weight, do you report just an average or full GPC chromatograms with PDI?
2. Batch-to-Batch Consistency
Request historical COA data for the same specification over the last 6-12 months. Calculate the coefficient of variation for key parameters (assay, protein, MW). A well-controlled supplier maintains CV <5% for molecular weight and <20% for protein residuals.
3. Certification Portfolio
ISO 13485 (medical devices), cGMP, DMF filing, COSMOS (organic cosmetics), HALAL, KOSHER — each certification requires specific quality systems that indirectly ensure purity control. The more certifications a supplier holds, the more robust their quality infrastructure.
4. Traceability
Can the supplier trace any batch back to its fermentation lot, raw material sources, and testing records? Full traceability is essential for investigating quality issues and conducting recalls if necessary.
5. Transparency
A trustworthy supplier provides:
· Full COA with all parameters, not just a selection
· GPC chromatograms on request
· Method descriptions alongside results
· Willingness to allow third-party testing
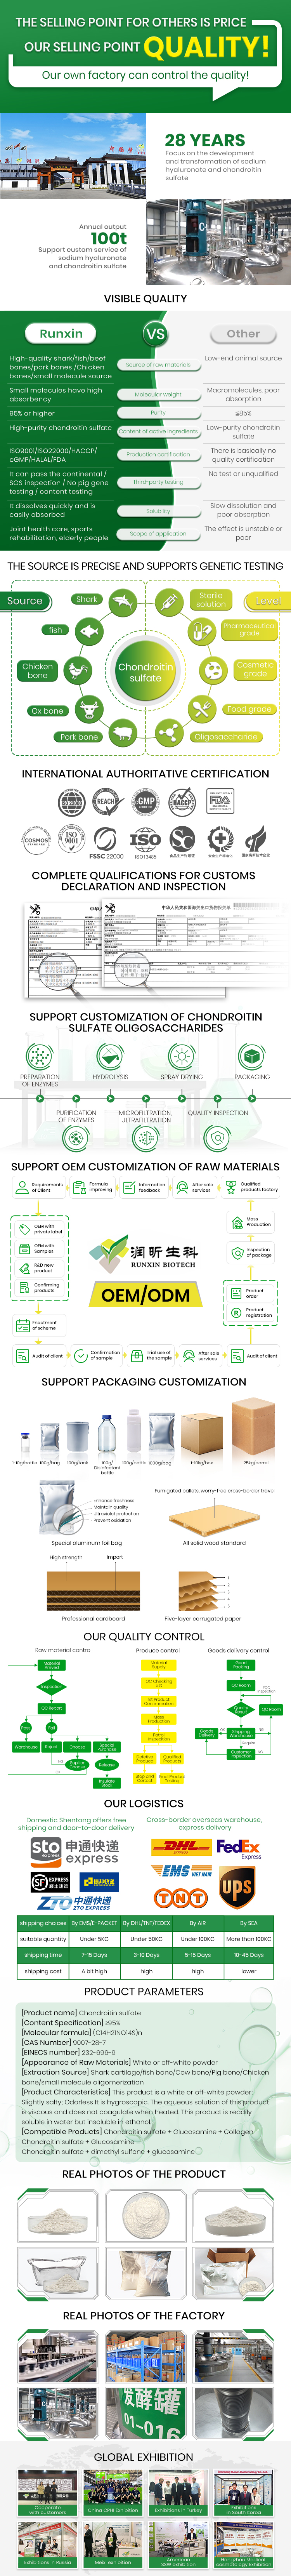
Suppliers like Shandong Runxin Biotechnology demonstrate comprehensive purity control across all five dimensions. With 28 years of dedicated microbial fermentation expertise, Runxin uses Bradford method for protein residuals (LOQ 0.005%), GPC-MALS for complete molecular weight characterization, LAL for endotoxin testing, and ICP-MS for full heavy metal screening — on every batch, every time. Their multi-certification portfolio (ISO 13485, CE, DMF 036368, COSMOS, HALAL, cGMP) and export experience across 34 countries reflect a quality system built for the most demanding applications.
Summary: Purity Is a Framework, Not a Number
Sodium hyaluronate purity encompasses chemical identity, biological safety, and chemical impurity control — each requiring specific analytical methods and acceptance criteria. The "right" purity level depends on your application:
· Topical cosmetics: Focus on protein residuals (≤0.1%), microbial limits, and heavy metals
· Food supplements: Tighter heavy metal limits, additional pathogen testing
· Ophthalmic / injectable: Endotoxin is non-negotiable, protein ≤0.05%, full pharmacopoeia compliance
· Post-procedure / sensitive skin: Treat as pharmaceutical-grade even if the application is technically cosmetic
When evaluating suppliers, don't just compare prices and assay percentages. Look at the complete purity profile, the testing methods behind it, and the consistency of those results across batches. Purity is what separates a reliable raw material from a quality surprise waiting to happen.
Need high-purity sodium hyaluronate with full transparency on testing? Contact Runxin Biotechnology for detailed COAs and specifications tailored to your application.